

In the realm of industrial infrastructure, moisture cables play a pivotal role in ensuring the seamless operation of various systems. As a dedicated moisture cable supplier, I often encounter inquiries about industry certifications for these essential components. This blog post aims to delve into the topic, exploring the significance of certifications, the types of certifications available, and how they impact the quality and reliability of moisture cables.
The Significance of Industry Certifications
Industry certifications serve as a testament to a product's compliance with established standards and regulations. For moisture cables, these certifications are crucial as they provide assurance to customers that the cables meet specific performance criteria, ensuring their suitability for intended applications.
Certifications offer several benefits. Firstly, they enhance the credibility of the product and the supplier. When a moisture cable is certified, it demonstrates that the manufacturer has met rigorous testing and evaluation processes, which can instill confidence in potential buyers. Secondly, certifications can help in differentiating products in a competitive market. A certified moisture cable may be perceived as a higher - quality option compared to non - certified alternatives, giving it an edge in the marketplace.

Types of Industry Certifications for Moisture Cables
International Electrotechnical Commission (IEC) Standards
The IEC is an international organization that develops and publishes standards for electrical, electronic, and related technologies. Many moisture cables are tested against IEC standards. For example, IEC 60228 defines the requirements for conductors of insulated cables. This standard specifies the characteristics of conductors, such as their cross - sectional area, resistance, and material composition. A moisture cable that complies with IEC 60228 is likely to have conductors that are of high quality and suitable for electrical transmission.
IEC also has standards related to environmental performance. IEC 60529, known as the Ingress Protection (IP) code, classifies the degree of protection provided by enclosures of electrical equipment against the intrusion of solid objects (including dust) and water. Moisture cables with a high IP rating, such as IP67 or IP68, are well - protected against water ingress, making them suitable for use in wet or humid environments.
National Electrical Code (NEC)
In the United States, the NEC is a widely recognized standard for electrical installations. While the NEC does not specifically certify moisture cables, it provides guidelines on the installation and use of electrical wiring, including cables in damp or wet locations. Cables used in these areas must meet certain requirements to ensure safety. For instance, cables installed in wet locations must have a moisture - resistant outer jacket.
Underwriters Laboratories (UL) Certifications
UL is a global safety science company that offers a range of certifications for electrical products. UL 1581 is a standard for electrical wires, cables, and flexible cords. Cables that are UL 1581 - listed have undergone testing for various properties, such as flammability, mechanical strength, and electrical performance. A moisture cable with a UL 1581 listing indicates that it has met the safety and performance requirements set by UL.
ISO 9001
ISO 9001 is a quality management system standard developed by the International Organization for Standardization (ISO). While it is not a product - specific certification, it is relevant for moisture cable suppliers. A supplier with an ISO 9001 certification has a documented quality management system in place, which means that they have processes for ensuring consistent product quality, from raw material sourcing to final product delivery. This can give customers confidence in the overall quality of the moisture cables supplied.
Industry Certifications and Product Applications
Industrial Automation
In industrial automation settings, moisture cables are used to connect sensors, actuators, and control systems. These cables need to be reliable and resistant to moisture to ensure the proper functioning of the automation equipment. Certifications such as IEC standards and UL listings are particularly important in this application. For example, a moisture - resistant cable with a high IP rating can be used in a factory environment where there may be water or steam present.
Grain Storage
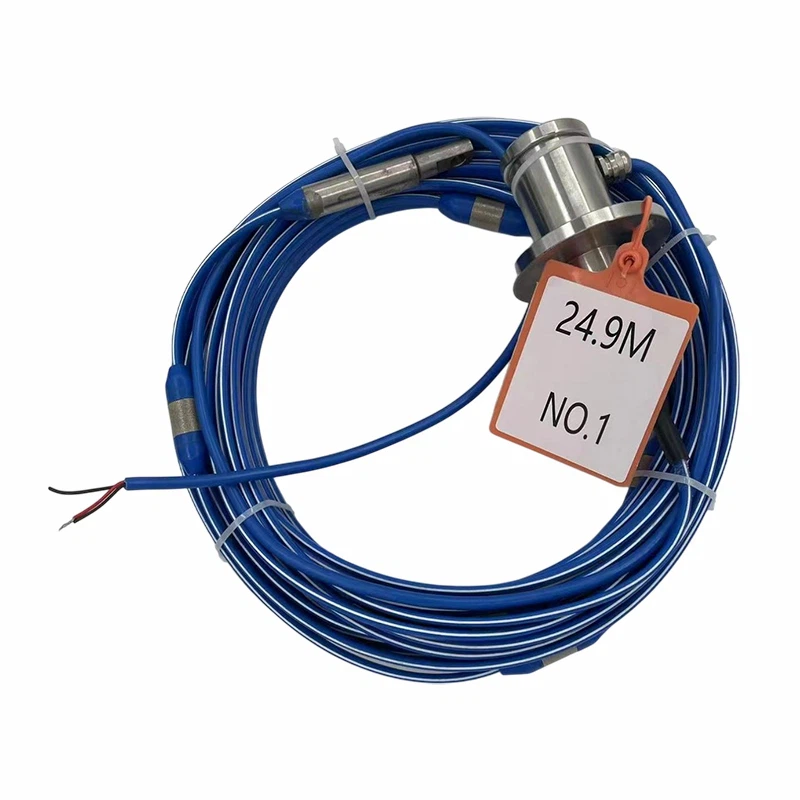
In the grain storage industry, moisture cables are used for monitoring the temperature and humidity inside grain silos. The Dedicated Temperature And Humidity Sensor Cable For Grain Silos and High - Precision Grain Condition Temperature And Humidity Measurement Cable are specifically designed for this purpose. Certifications related to accuracy and reliability are crucial here. A cable that meets relevant IEC standards for measurement accuracy can provide accurate data on grain conditions, helping to prevent spoilage and ensure the quality of stored grain.
Outdoor and Marine Applications
For outdoor and marine applications, moisture cables are exposed to harsh environmental conditions, including saltwater, rain, and high humidity. Certifications like the IP rating are essential to ensure that the cables can withstand these conditions. A Moisture - proof Cable with a high IP rating and compliance with relevant corrosion - resistance standards can be used in coastal areas or on ships.
How Our Moisture Cables Meet Industry Certifications
As a moisture cable supplier, we are committed to providing high - quality products that meet or exceed industry standards. Our manufacturing processes are designed to ensure that every cable we produce is of the highest quality.
We source raw materials from reputable suppliers and conduct strict quality control checks at every stage of the manufacturing process. Our cables are tested against multiple industry standards, including IEC, UL, and NEC requirements. For example, our cables undergo IP rating testing to ensure their resistance to water ingress, and conductor testing to meet IEC 60228 standards.
We also hold an ISO 9001 certification, which reflects our commitment to quality management. This certification ensures that our processes are well - defined and continuously improved, resulting in consistent product quality.
Conclusion and Call to Action
Industry certifications are an important aspect of moisture cables, providing assurance of quality, reliability, and compliance with standards. Whether you are in the industrial automation, grain storage, or outdoor and marine industries, choosing a certified moisture cable is crucial for the success of your projects.
As a leading moisture cable supplier, we offer a wide range of certified moisture cables that are suitable for various applications. Our commitment to quality and compliance with industry standards ensures that you get the best - performing cables for your needs.
If you are interested in learning more about our moisture cables or would like to discuss your specific requirements, we encourage you to contact us for a detailed consultation. Our team of experts is ready to assist you in finding the right moisture cable solution for your project.
References
- International Electrotechnical Commission (IEC) official documentation
- National Electrical Code (NEC) publications
- Underwriters Laboratories (UL) standards and related materials
- ISO 9001 official guidelines